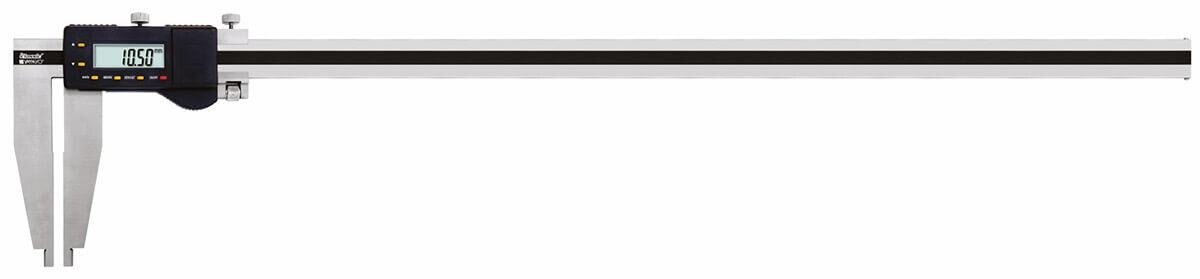
A “heavy duty” label does not tell you whether a caliper is accurate enough for a drawing tolerance, durable enough for coolant exposure, or suitable for a 500 mm workpiece. You will be able to compare models by measurable specifications, select the right instrument for the geometry and tolerance, and set up checks that produce repeatable production readings.
Key takeaways
- Compare jaw reach, beam rigidity, resolution, accuracy and protection rating.
- Match jaw geometry to outside diameters, wall thickness and deep steps.
- Control force, alignment, temperature and zeroing for repeatable cell readings.
- Request calibration records, data-output details, warranty terms and local service support.
Which specifications separate heavy-duty digital caliper models?
A fair model comparison starts with measured performance, not the label “heavy duty” or a 0.01 mm display. For heavy duty digital calipers for comparison in Mumbai, record the same specifications for every model.
| Specification | Record | Why it matters |
|---|---|---|
| Measuring capacity | Maximum and minimum range | Confirms coverage of the part |
| Resolution | 0.01 mm or 0.001 mm | Shows display increment, not accuracy |
| Maximum permissible error | Limit over a stated span | Defines the instrument’s measurement error |
| Repeatability | Repeated-reading variation | Shows consistency between readings |
| Jaw length and thickness | Dimensions and contact design | Affects reach, stiffness and access |
| Beam construction | Material, section and rigidity | Indicates resistance to bending |
| Overall length and mass | Complete instrument values | Predicts handling and storage needs |
| Working-range error | Error at the actual span used | Prevents relying on one nominal-size result |
ISO 13385-1:2019 is the relevant reference for caliper design and metrological characteristics. A 0.001 mm display does not make a caliper more accurate than a 0.01 mm model; compare maximum permissible error and repeatability instead.
In a digimatic caliper comparison, treat 300 mm and 500 mm models as alignment-sensitive instruments. Longer beams and larger jaws deflect more, so require the manufacturer’s error specification at your actual measurement span, not only at 150 mm.
Ask for a calibration result or specification showing the range and error limits; a certificate reporting one nominal size is insufficient.
Which caliper suits outside diameters, wall thickness and deep steps?
Match the caliper to the contact geometry, not merely the part’s nominal diameter.
Large pipe and shaft outside diameters need a range and jaw opening that clear the feature; wall thickness needs jaws that reach an accessible cut edge; internal dimensions need parallel inside faces; deep steps and recesses need sufficient jaw reach and depth-rod travel.
| Type | Main advantage | Best production use | Limitation |
|---|---|---|---|
| Heavy-duty digital | Fast, clear readings and possible data capture | Large outside diameters, accessible wall thickness, internal spans and steps | Batteries, contamination and proprietary data interfaces |
| Standard digital | Compact and economical | Small, clean parts with moderate range | Less beam stiffness and capacity |
| Heavy-duty vernier | Mechanical simplicity and no battery dependence | Harsh cells where a direct scale reading is acceptable | Slower reading and manual recording |
| Solid-type vernier | Rigid beam with strong resistance to slider play | Large parts and repeated shop-floor measurement | Heavier, slower and without automatic data output |
For digital calipers for manufacturing, check jaw length, jaw thickness, beam rigidity, slider movement and depth capacity. A long beam that flexes, or jaws that do not seat squarely, can produce a confident but false reading.
Choose a micrometer or dedicated comparative gauge for close-tolerance outside dimensions when caliper error, force variation or alignment uncertainty approaches the drawing tolerance. A caliper measures accessible dimensions without cutting the part; it does not reveal internal or subsurface defects. Use ultrasonic, radiographic, magnetic-particle, dye-penetrant or eddy-current testing for that purpose.
Before buying a heavy duty digital caliper in mumbai, trial it on representative pipes, shafts and recessed parts rather than judging the “heavy duty” label alone.
How do you produce repeatable readings in a production cell?
Repeatability starts with the contact surfaces, not the display. Clean the caliper faces and workpiece, remove casting flash and burrs, and check jaw alignment and parallelism before measuring. Square the jaws to the feature, apply consistent moderate force, and avoid rocking the slider.
- For a flat fabricated surface, contact the intended planes rather than an edge or weld bead.
- For a pipe, keep the jaws square to the diameter; curved contact can produce a false reading if the jaws touch at an angle.
- Hold the slider steady, or lock it after positioning, then read the display without shifting the caliper.
- Repeat the measurement at least twice and investigate a changing result instead of averaging it away.
Common causes of variation deserve a recorded correction:
| Cause | False result | Corrective action |
|---|---|---|
| Dirt between faces | Reading too large | Clean faces and workpiece |
| Burr or weld spatter | Localised high reading | Remove burr, then remeasure |
| Skewed or non-parallel jaws | Size changes as the caliper rocks | Align square and check parallelism |
| Excessive force | Distorted contact or workpiece | Use moderate, repeatable pressure |
| Wrong geometric surfaces | Consistent but irrelevant size | Mark the drawing feature before measuring |
Run a short repeatability study with three operators taking repeated readings on representative castings, pipes and fabricated parts. Record each value, the range and the feature location; a calibration certificate at one nominal size cannot reveal operator technique or curved-pipe errors.
Allow the part and caliper to equilibrate near 20 °C before close-tolerance work. A 300 mm steel dimension changes roughly 0.017 mm across a 5 °C difference. Include this control in any digimatic caliper comparison or evaluation of digital calipers for manufacturing.
How do accuracy, calibration and data features affect the buying decision?
A caliper is adequate only when its maximum permissible error and repeatability fit the drawing tolerance or process-control limit, including your allowed decision uncertainty. Do not divide tolerance by the displayed increment: 0.01 mm or 0.001 mm resolution does not establish accuracy.
| Feature | Compare | Buying implication |
|---|---|---|
| Maximum permissible error | Stated over the working range, not at one size | Reject a model whose error consumes the decision margin |
| Repeatability | Repeated readings on the actual feature | Investigate operator technique or choose a tighter instrument if results scatter |
| Display and zero | Readability, one-touch zero-setting, zero stability | A clear display and stable zero reduce acceptance mistakes |
| Survival and cleaning | Battery life, shock resistance, jaw durability and cleanable surfaces | Coolant residue and dropped tools expose weak designs |
| Data output | Proprietary protocol, connector, cable, wireless gateway, software compatibility, decimal format, and transmission of zero or hold states | Confirm the complete workflow before buying digital calipers for manufacturing |
For a digimatic caliper comparison, verify size with gauge blocks or a certified reference at several points across the working range. Record as-found results, check zero stability, and remove the instrument from service when error exceeds the acceptance limit, readings drift, jaws are damaged, or the caliper suffers a shock.
Set calibration intervals from usage rate, coolant exposure, handling, history, drift and decision risk; ISO/IEC 17025 describes calibration-laboratory competence, not a universal interval. In Mumbai, inspect battery contacts, scale, fasteners and data connector for humidity and coolant residue.
IP67 means dust protection and temporary immersion under IEC 60529 test conditions, not resistance to coolant chemistry, washdown pressure or corrosion.
What should you verify with an industrial caliper supplier in Mumbai?
A low purchase price becomes expensive when a damaged jaw, missing cable or overdue calibration stops a production cell. Ask an industrial caliper supplier in Mumbai for this procurement record before placing the order:
- Exact model, measuring range and stated maximum permissible error over the range, not only the display resolution.
- Calibration certificate identifying traceability, reference standards, date, as-found results and error limits.
- Acceptance readings at sizes that match your work: pipe outside diameters, casting steps or fabricated-part thicknesses.
- Stock status and lead time for replacement jaws, batteries, data cables and any proprietary interface gateway.
- Repair process, expected turnaround, loaner policy and the location handling the work.
- Local calibration arrangements, including pickup, return and adjustment charges.
| Support option | Production consequence | Evidence to request |
|---|---|---|
| Lowest-price import | A failed instrument waits for parts or overseas service | Written parts lead time and repair route |
| Supported heavy-duty digital caliper in Mumbai | Faster recovery and controlled measurement records | Local calibration plan, accessories and turnaround |
| Supplier trial and acceptance | Geometry or data-transfer faults appear before installation | Trial readings on representative pipes, castings or fabricated parts |
Ask Yamayo Instruments whether it can document calibration, supply accessories, arrange repairs and run that measurement trial for the selected model. Before approval, record the measured feature, drawing tolerance, required range, error limit, coolant or humidity exposure, and data workflow, including cable, gateway, software and transmitted zero or hold status.
Related product
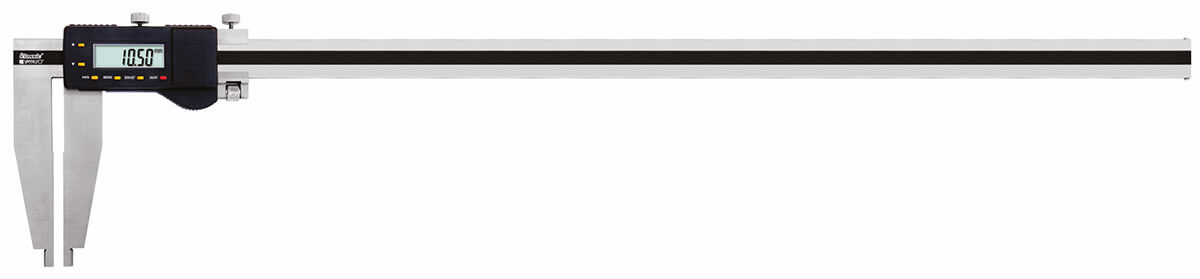 | Calipers Heavy Duty Digimatic Calipers The Heavy Duty Digimatic Caliper is a large-capacity precision digital measuring instrument designed for accurate... View product → |
Frequently asked questions
Which specifications separate heavy-duty digital caliper models?
Compare stated accuracy across the measuring range, resolution, jaw length and thickness, beam rigidity, depth capacity, IP protection rating, battery life and data-output method. Check whether the maker states performance under a defined temperature, contact force and measurement condition.
Which caliper suits outside diameters, wall thickness and deep steps?
Use broad outside jaws for external diameters, thin knife-edge or dedicated step jaws for wall thickness, and a long, rigid depth rod or depth base for deep steps. Confirm the jaw shape and reach against the actual part drawing instead of choosing by range alone.
How do you produce repeatable readings in a production cell?
Clean the contact faces and part, zero the caliper, align the jaws squarely, use consistent closing force and keep the instrument and workpiece at a stable temperature. Train operators to use the same datum and record the part number, instrument ID and reading.
How do accuracy, calibration and data features affect the buying decision?
Select accuracy that supports the part tolerance, then confirm the calibration interval, traceability, certificate format and out-of-tolerance process. Choose data output only when it reduces transcription errors or supports inspection records; verify connector, protocol, software and integration requirements.
What should you verify with an industrial caliper supplier in Mumbai?
Ask for the exact model datasheet, accuracy table, IP rating, jaw and depth dimensions, calibration certificate options, replacement parts, warranty, lead time and local service process. Confirm stock, inspection before dispatch and support for data connectivity when buying digital calipers for manufacturing.