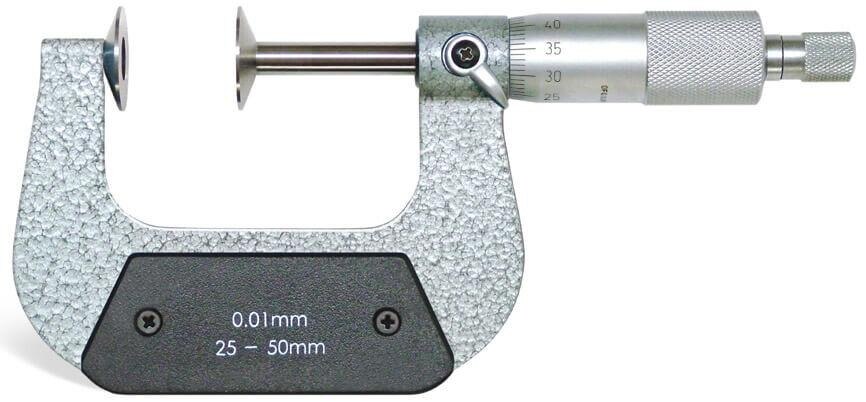
The words point micrometer and disc micrometer describe different contact geometries, so a quotation can easily deliver the wrong tool for your part. You will be able to identify the feature, choose the correct instrument type, take repeatable readings, and verify whether a Chennai listing matches your required range, accuracy, and stock condition.
Key takeaways
- Use disc faces for gear teeth, webs, blades, and thin edges.
- Use pointed contacts for narrow grooves, keyways, slots, and drill webs.
- Check zero, contact-face condition, calibration status, and measuring range before inspection.
- Request resolution, accuracy, stock status, and calibration documents in the quotation.
Choose the Contact Geometry Before You Request a Quote
Choose a disc micrometer when circular faces must reach a gear-tooth feature, root tangent, thin section, shoulder, web, blade, or sheet edge that flat faces would bridge. Choose a pointed or conical point micrometer for machinery when the contact must reach the bottom of a narrow groove, keyway, slot, recess, or drill web.
| Option | Contact geometry | Best match |
|---|---|---|
| Disc micrometer | Circular measuring faces | Gear roots, shoulders, webs, blades, thin sections, and sheet edges |
| Point micrometer | Pointed or conical contacts | Narrow grooves, keyways, slots, recesses, and drill webs |
| Standard outside micrometer | Broad flat faces | Accessible ordinary outside dimensions |
Do not treat point and disc micrometers as interchangeable search terms. A pointed contact can indent soft sheet or flexible material, while a disc face can be too broad for a narrow slot. A search for point micrometer disc micrometers in chennai can therefore combine two different tool families.
Read the drawing before requesting a quote. Identify whether it specifies:
- Gear root tangent measurement
- Groove width or diameter
- Shoulder access
- Drill-web thickness
- An ordinary outside dimension
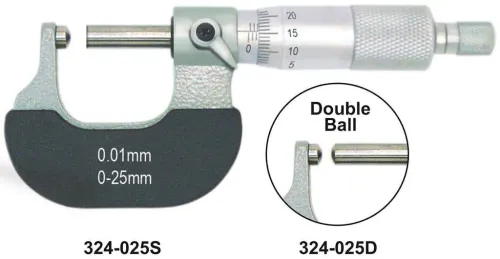
Then check spindle travel, frame range, throat depth, disc diameter, disc thickness, and contact shape. A nominal 0–25 mm range does not prove that the discs can enter your feature.
For gear work, confirm the tooth form, helix angle, disc geometry, and specified measurement method. A disc micrometer is not automatically a replacement for span measurement, over-pins measurement, or a dedicated gear inspection method.
Take a Disc-Micrometer Reading Without Bridging or Tilting
For gears, splines, grooves, and narrow shoulders, take the reading only after both discs sit fully on the specified contact surfaces. A disc micrometer in Chennai is useful here because its circular faces can reach features that flat anvils bridge, but alignment still controls the result.
- Wipe the disc faces and the part with a lint-free cloth. Remove chips, abrasive dust, oil film, and raised burrs without rounding the feature.
- Open the spindle enough to clear the part. Position both discs on the intended surfaces, never on a gear flank, damaged tooth edge, burr, or adjacent shoulder.
- Keep the frame square to the feature and align the spindle axis with the dimension shown on the drawing.
- Close the spindle with the ratchet or friction thimble until the specified measuring force is reached. Do not tighten by hand or rock the frame to find a lower value.
- On foil, paper, shim, sheet, or blade, control force carefully; excess pressure compresses the material and creates a measurement-force error.
- Repeat readings at the required teeth or positions on gears and splines. Record the part number, location, temperature, and instrument identification, then compare the spread between readings.
| Setup | Correct practice | What goes wrong |
|---|---|---|
| Disc contact | Full contact on the intended surfaces | Edge contact produces a false dimension |
| Frame position | Square, with the spindle axis aligned | Tilting changes the contact geometry |
| Measuring force | Ratchet or friction thimble | Hand force compresses flexible material |
Verify Zero, Contact Faces, and Calibration Before Inspection
Trust the reading only after checking zero against the correct reference condition. Close clean measuring faces fully, or follow the manufacturer’s specified zeroing procedure when offset or non-contacting disc geometry prevents ordinary face-to-face closure. An indicated zero alone does not prove calibration.
1. Clean both discs and inspect them for nicks, flat spots, corrosion, looseness, and embedded chips. Inspect pointed contacts for bent tips, worn points, or damage.
2. Check the micrometer against a certified gauge block, setting standard, or reference close to the dimension you will inspect. Record the nominal value, indicated value, temperature, instrument identification, and date.
3. Request the maker’s accuracy specification over the full range, maximum permissible error, repeatability, calibration interval, and calibration certificate. A digital display resolving 0.001 mm is not necessarily accurate to 0.001 mm; a mechanical micrometer reading 0.01 mm can be adequate when the part tolerance allows it.
4. Bring the part and micrometer near 20 °C before precision comparison. A hot part, hand-heated frame, or temperature difference between them changes dimensions through thermal expansion.
5. Remove the instrument from service for adjustment or calibration when zero exceeds the maker’s limit, reference readings exceed the stated error, repeated readings drift, contact faces are damaged, or the micrometer has been dropped.
Keep the recorded reference result with the inspection record. A clean display cannot correct a damaged contact, incorrect zeroing method, or thermal error.
Compare Mechanical, Digital, and Alternative Measuring Methods
The fastest reliable method is the one whose contact geometry and uncertainty match the drawing, not the one with the most advanced display. A mechanical disc micrometer avoids batteries and electronic contamination concerns; its 0.01 mm reading is adequate when the tolerance supports it.
A digital or Digimatic model improves readability, speed, and data recording, but 0.001 mm resolution is not 0.001 mm accuracy.
| Option | Strength | Check before choosing |
|---|---|---|
| Mechanical disc micrometer | No battery; 0.01 mm reading | Confirm tolerance, repeatability, and calibration |
| Digital disc micrometer | 0.001 mm display; easier recording | Compare accuracy, battery life, data output, IP protection, and resistance to coolant, oil, and chips |
| Standard outside micrometer | Fast for accessible cylindrical outside dimensions | Do not use it on recessed shoulders or narrow gear features |
| Vernier caliper | Quick broad checks | Contact force is less controlled and jaws can bridge small features |
Use a blade micrometer for thin blades or narrow grooves, and a point micrometer for the bottom of a small groove, keyway, or slot. Do not use a point on soft flexible sheet; it can indent the material.
For gear drawings that specify tooth thickness, span, or a formal inspection method, use a gear-tooth vernier, span micrometer, over-pins measurement, or dedicated gear measuring machine. A disc micrometer is not a universal replacement.
Treat digital disc micrometer availability as a model-specific question: contact geometry, measuring-face size, force control, data output, and protection matter more than the display alone.
Check Chennai Stock, Specification, and the Supplier’s Quotation
State the feature and measurement method before asking for a price. A search for “point micrometer disc micrometers in Chennai” can combine two different tool families.
| Option | Contact geometry | Appropriate use |
|---|---|---|
| Pointed-anvil micrometer | Pointed or conical contacts | Groove bottoms, keyways, slots, drill webs |
| Disc-anvil micrometer | Circular disc faces | Root tangents, shoulders, thin sections, webs |
Ask the disc micrometer supplier for:
- Exact model number, range, spindle travel, disc diameter, disc thickness, contact geometry, and stated accuracy over the full range
- Resolution, measuring-force control, output interface, protection rating, calibration certificate, warranty, and replacement-battery details
- Confirmation that the quotation covers a pointed-anvil micrometer, a disc-anvil micrometer, or both
Treat digital disc micrometer availability as model-specific. Ask for the live stock location, dispatch lead time, and confirmation that the item is physically in Chennai rather than an imported order.
If the quotation lists only a nominal 0–25 mm capacity, request a photograph or manufacturer datasheet; disc size, thickness, and throat access can decide whether the instrument reaches your part.
Yamayo Instruments can help a Chennai manufacturing or inspection team compare contact geometry, range, calibration documentation, and application before procurement. Attach the drawing, tolerance, sample component, and required inspection record to the enquiry, so the quoted instrument is judged on measurement capability rather than price alone.
Related products
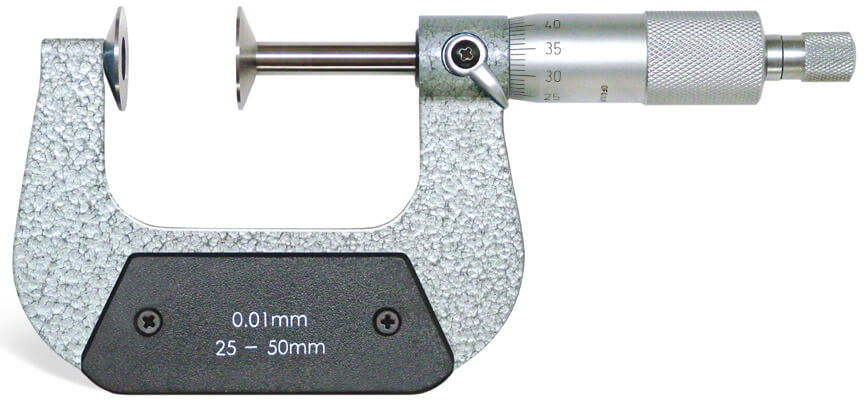 | Micrometers Disc Micrometers The Disc Micrometer is a specialized precision measuring instrument designed for measuring the root tangent length of spur gears,... View product → |
 | Micrometers Point Outside Micrometers The Point Outside Micrometer is a specialized precision measuring instrument designed for measuring web thickness of... View product → |
Frequently asked questions
When should you choose a disc micrometer instead of a point micrometer?
Choose a disc micrometer when circular faces must reach a gear-tooth feature, root tangent, thin section, shoulder, web, blade, or sheet edge. Choose a pointed or conical point micrometer when the contact must reach the bottom of a narrow groove, keyway, slot, recess, or drill web.
How do you take a disc-micrometer reading without bridging or tilting?
Place the disc faces squarely against the feature, use the ratchet or friction thimble for consistent force, and check that both contacts seat on the intended surfaces rather than bridging an edge.
What should you verify before using a point or disc micrometer for inspection?
Check the zero setting, contact faces, measuring range, resolution, accuracy specification, calibration status, and calibration certificate before recording inspection results.
What should a Chennai disc micrometer quotation include?
Ask for the exact contact geometry, range, resolution, accuracy, mechanical or digital display type, calibration documentation, stock status, delivery time, and applicable taxes or charges.